How High Inspection Pass Rates Are Achieved in High-Volume Appliance Manufacturing
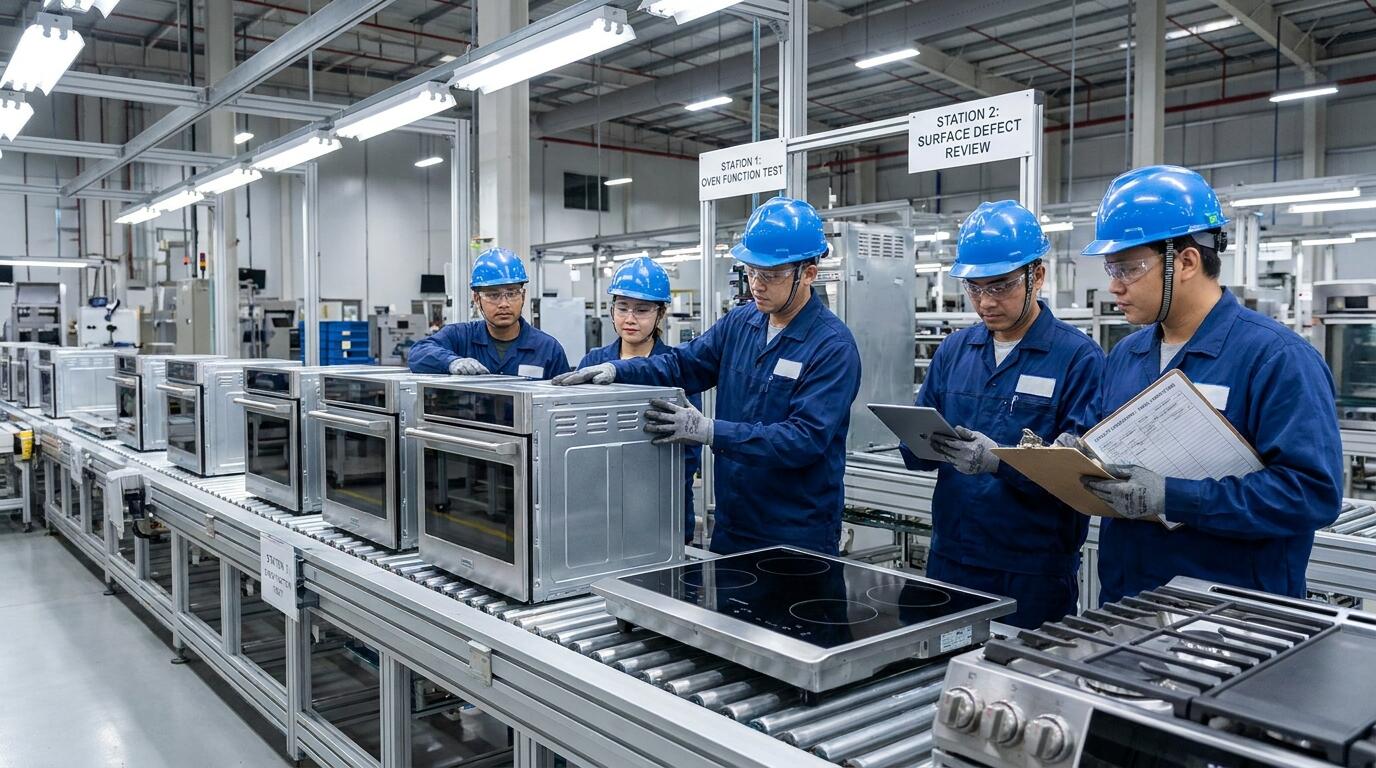
ALT: Quality inspection team reviewing smart kitchen appliances on a high-volume OEM manufacturing line
Why Inspection Pass Rates Define the Future of High-Volume Appliance Manufacturing
Consistently high inspection pass rates in high-volume appliance manufacturing are not achieved by accident; they are the result of layered quality systems, disciplined process control, and a manufacturing culture that treats defect prevention as a core business function rather than an afterthought. As global B2B buyers tighten their sourcing standards and become less tolerant of field failures, an OEM/ODM factory's ability to sustain near-perfect first-pass yields has become a decisive differentiator.
In our work with international procurement teams, a pattern we consistently see is that buyers conflate "final inspection" with "quality assurance." These are not the same thing. Final inspection catches defects; a true quality system prevents them. This article breaks down the specific mechanisms — from incoming material gatekeeping to statistical process control to multi-stage audit protocols — that allow a disciplined manufacturer to maintain exceptional inspection pass rates even at scale. Understanding these mechanisms is essential for any sourcing manager evaluating a potential OEM partner in the smart kitchen appliance sector.
Three core points frame this discussion: first, that high pass rates depend on upstream prevention, not downstream sorting; second, that traceability and data systems are what make prevention repeatable; and third, that the right manufacturing partner will openly demonstrate these systems rather than simply claim compliance.
Who This Guide Is For — and Where It Applies
Applicable Scenarios:
- Importers and private-label brands sourcing smart kitchen appliances — including ranges, ovens, cooktops, and dishwashers — from Chinese OEM/ODM manufacturers who need to evaluate factory quality capability before committing to large purchase orders
- Procurement managers designing supplier qualification frameworks and needing a technical reference point for what "rigorous quality" actually looks like inside a modern appliance factory
- Retailers and product developers working on custom or branded appliance lines who want to understand how manufacturing quality translates into lower warranty costs and stronger brand reputation
Not Applicable / Cautions:
- This guide focuses on manufactured goods quality systems at the factory level; it does not cover post-market surveillance, in-field service networks, or retail returns management, which require separate frameworks
- Buyers sourcing from brokers or trading companies (rather than direct factories) will find that many of the quality levers described here are outside the trading company's control — a critical risk factor that is often underestimated
The High-Stakes Problem With Quality at Scale
Maintaining inspection quality in high-volume manufacturing is fundamentally different from maintaining it in small-batch or prototype production. When a factory produces tens of thousands of appliance units per month, even a small process drift — a slightly worn die, a batch of inconsistent components, a subtle calibration shift in an automated welder — can propagate through thousands of units before it is detected. The cost implications are severe: rework, scrap, delayed shipments, and, worst of all, field failures that damage end-customer trust and retailer relationships.
While many appliance manufacturers hold quality management system certifications such as ISO 9001, holding a certificate alone does not guarantee consistent execution on the factory floor. What separates manufacturers that sustain high inspection pass rates from those that merely pass periodic audits is the gap between documented compliance and daily operational capability under high-volume production pressure.
In the smart kitchen appliance segment specifically, complexity has increased substantially. Products like connected ranges, sensor-equipped cooktops, and electronically controlled ovens combine mechanical fabrication, electrical assembly, firmware integration, and industrial design — four distinct quality disciplines that must be coordinated within a single production flow. A defect can originate in any one of these layers and may not manifest until the product is in a customer's hands. This is precisely why the quality infrastructure behind a claimed high inspection pass rate deserves careful scrutiny from any B2B buyer.
The Engineering Architecture Behind High Inspection Pass Rates
Building a Defect-Prevention System From the Ground Up
Step 1: Establish Incoming Material Quality Control as a Non-Negotiable Gate
Every defect that enters a factory through purchased components is a defect that the production line and inspection team must later detect and resolve — usually at much higher cost. Incoming Quality Control (IQC) is an important part of a manufacturer's quality management process. Buyers should ask suppliers whether they maintain approved vendor lists, document supplier performance, and apply appropriate Acceptance Quality Limit (AQL) sampling plans to incoming components. The sampling criteria and inspection procedures should be defined according to component type, product requirements, and applicable quality standards. The goal is to ensure that every subassembly, raw material, and bought-in component meets specification before it enters the value chain, not after.
Step 2: Embed In-Process Quality Controls at Every Critical Production Stage
Waiting until a finished product reaches the end-of-line inspection station to identify defects is a strategy that consistently fails at scale. High-performing factories design quality checkpoints directly into the production sequence — a practice known as in-process quality control (IPQC). For smart kitchen appliances, this typically includes dimensional checks during metal fabrication, weld integrity verification, electrical continuity and insulation resistance testing at the sub-assembly stage, firmware flashing and functional verification before enclosure is completed, and visual inspection for surface quality before packing. Each checkpoint is documented, with pass/fail results tied to the specific production batch and shift. When a checkpoint flags an anomaly, it triggers a defined response — not just rework of the visible defect, but investigation of root cause to prevent recurrence.
Step 3: Implement Statistical Process Control to Catch Drift Before It Becomes Failure
Statistical process control (SPC) is the discipline of using real-time data from the production process to detect when a process is drifting toward an out-of-control condition — before defects actually occur. Depending on the product and production process, manufacturers may monitor critical variables such as fastening torque, gas valve leakage, burner ignition performance, and electronic control board test results. Buyers should ask which parameters are monitored, how control limits are established, and whether production records are available for review. When a data point trends toward a control limit, the system signals operators and engineers to intervene. This proactive, data-driven approach is what allows a well-run factory to sustain high first-pass yields over long production runs rather than experiencing periodic quality collapses followed by reactive firefighting.
Comparing Quality System Architectures: What Separates High-Performing Manufacturers
Different OEM/ODM factories approach quality architecture in fundamentally different ways. The table below illustrates how three common manufacturing models compare across the dimensions most relevant to B2B buyers evaluating long-term sourcing partnerships. The following table presents an illustrative comparison of three common approaches to manufacturing quality management. Actual inspection performance depends on product complexity, process stability, supplier controls, inspection criteria, and the consistency of implementation at the factory level.
| Comparison Dimension | Reactive / Inspection-Only Model | Compliance-Focused Model | Prevention-Driven / SPC Model |
|---|---|---|---|
| Primary defect detection point | End-of-line final inspection | Multiple checkpoints, process-dependent | Embedded at every production stage |
| Use of statistical data | Minimal or none | Periodic reporting | Continuous, real-time monitoring |
| Incoming material gatekeeping | Basic visual check | AQL sampling, documented | Full IQC with vendor scorecards |
| Traceability | Limited | Batch-level | Unit-level or batch-level with full audit trail |
| Response to process anomaly | Rework after failure | Corrective action reports | Root cause analysis + preventive action |
| Typical first-pass yield | Variable, often low | Moderate and inconsistent | Potentially more consistent when properly implemented |
| Risk to B2B buyer | High: late detection, high rework cost | Medium: dependent on system discipline | Reduced process risk through preventive controls |
The prevention-driven model—which integrates IQC, IPQC, SPC, and final quality control (FQC) into a single, data-connected system—provides an architecture that helps improve process consistency and reduce recurring defects under the pressure of high-volume production schedules.
The Role of Traceability, Root Cause Analysis, and Continuous Improvement
Traceability as the backbone of quality accountability. A high inspection pass rate is only meaningful if the factory can explain, with data, why it was achieved — and can replicate that outcome order after order. Traceability practices vary by manufacturer and product type. Buyers should confirm whether suppliers maintain batch-level or unit-level records covering component information, production processes, inspection results, and relevant corrective actions. The available records should be sufficient to support defect investigation and quality accountability within the agreed traceability scope. When a defect does occur, traceability allows the quality team to isolate whether the issue is confined to a specific batch of components, a specific machine, a specific shift, or a systemic process parameter — dramatically compressing the time needed to contain and resolve the problem.
Root cause analysis as the mechanism that turns defects into permanent improvements. In our experience supporting global sourcing partnerships, the factories that sustain high pass rates over time are distinguished not by the absence of defects — no manufacturing process is perfect — but by the speed and rigor with which they close the loop when defects do occur. Disciplined root cause analysis (RCA), using structured methodologies such as the 5-Why approach or fishbone (Ishikawa) diagrams, ensures that corrective actions address the actual cause rather than the symptom. A factory that repairs a defective unit without understanding why it failed will see that failure pattern return. A factory that identifies worn tooling as a contributing factor, updates its maintenance procedures, and revises the relevant control plan can reduce the likelihood of similar defects recurring. The effectiveness of these actions should be verified through subsequent production monitoring and inspection records.
Continuous improvement systems that institutionalize learning. The ISO 9001 quality management framework requires organizations to address nonconformities, determine their causes, and implement appropriate corrective actions. Manufacturers can support continuous improvement by documenting corrective actions, reviewing their effectiveness, and updating relevant work instructions and control plans when necessary. Regular quality reviews at the line level, cross-functional defect analysis meetings, and formal engineering change processes that capture lessons learned into updated work instructions and control plans are the operational habits that separate consistently high-performing factories from those that achieve quality in bursts and lose it under production pressure.
Workforce competency and standardized work as quality enablers. Even the most sophisticated quality system will underperform if the people executing it are not adequately trained or if the work instructions they follow are inconsistently written. High-performing factories invest in detailed, visual work instructions at every critical process step, structured operator training with competency verification, and regular calibration of both measurement instruments and human judgment through reference samples and boundary samples (also called limit samples) for visual inspection criteria.
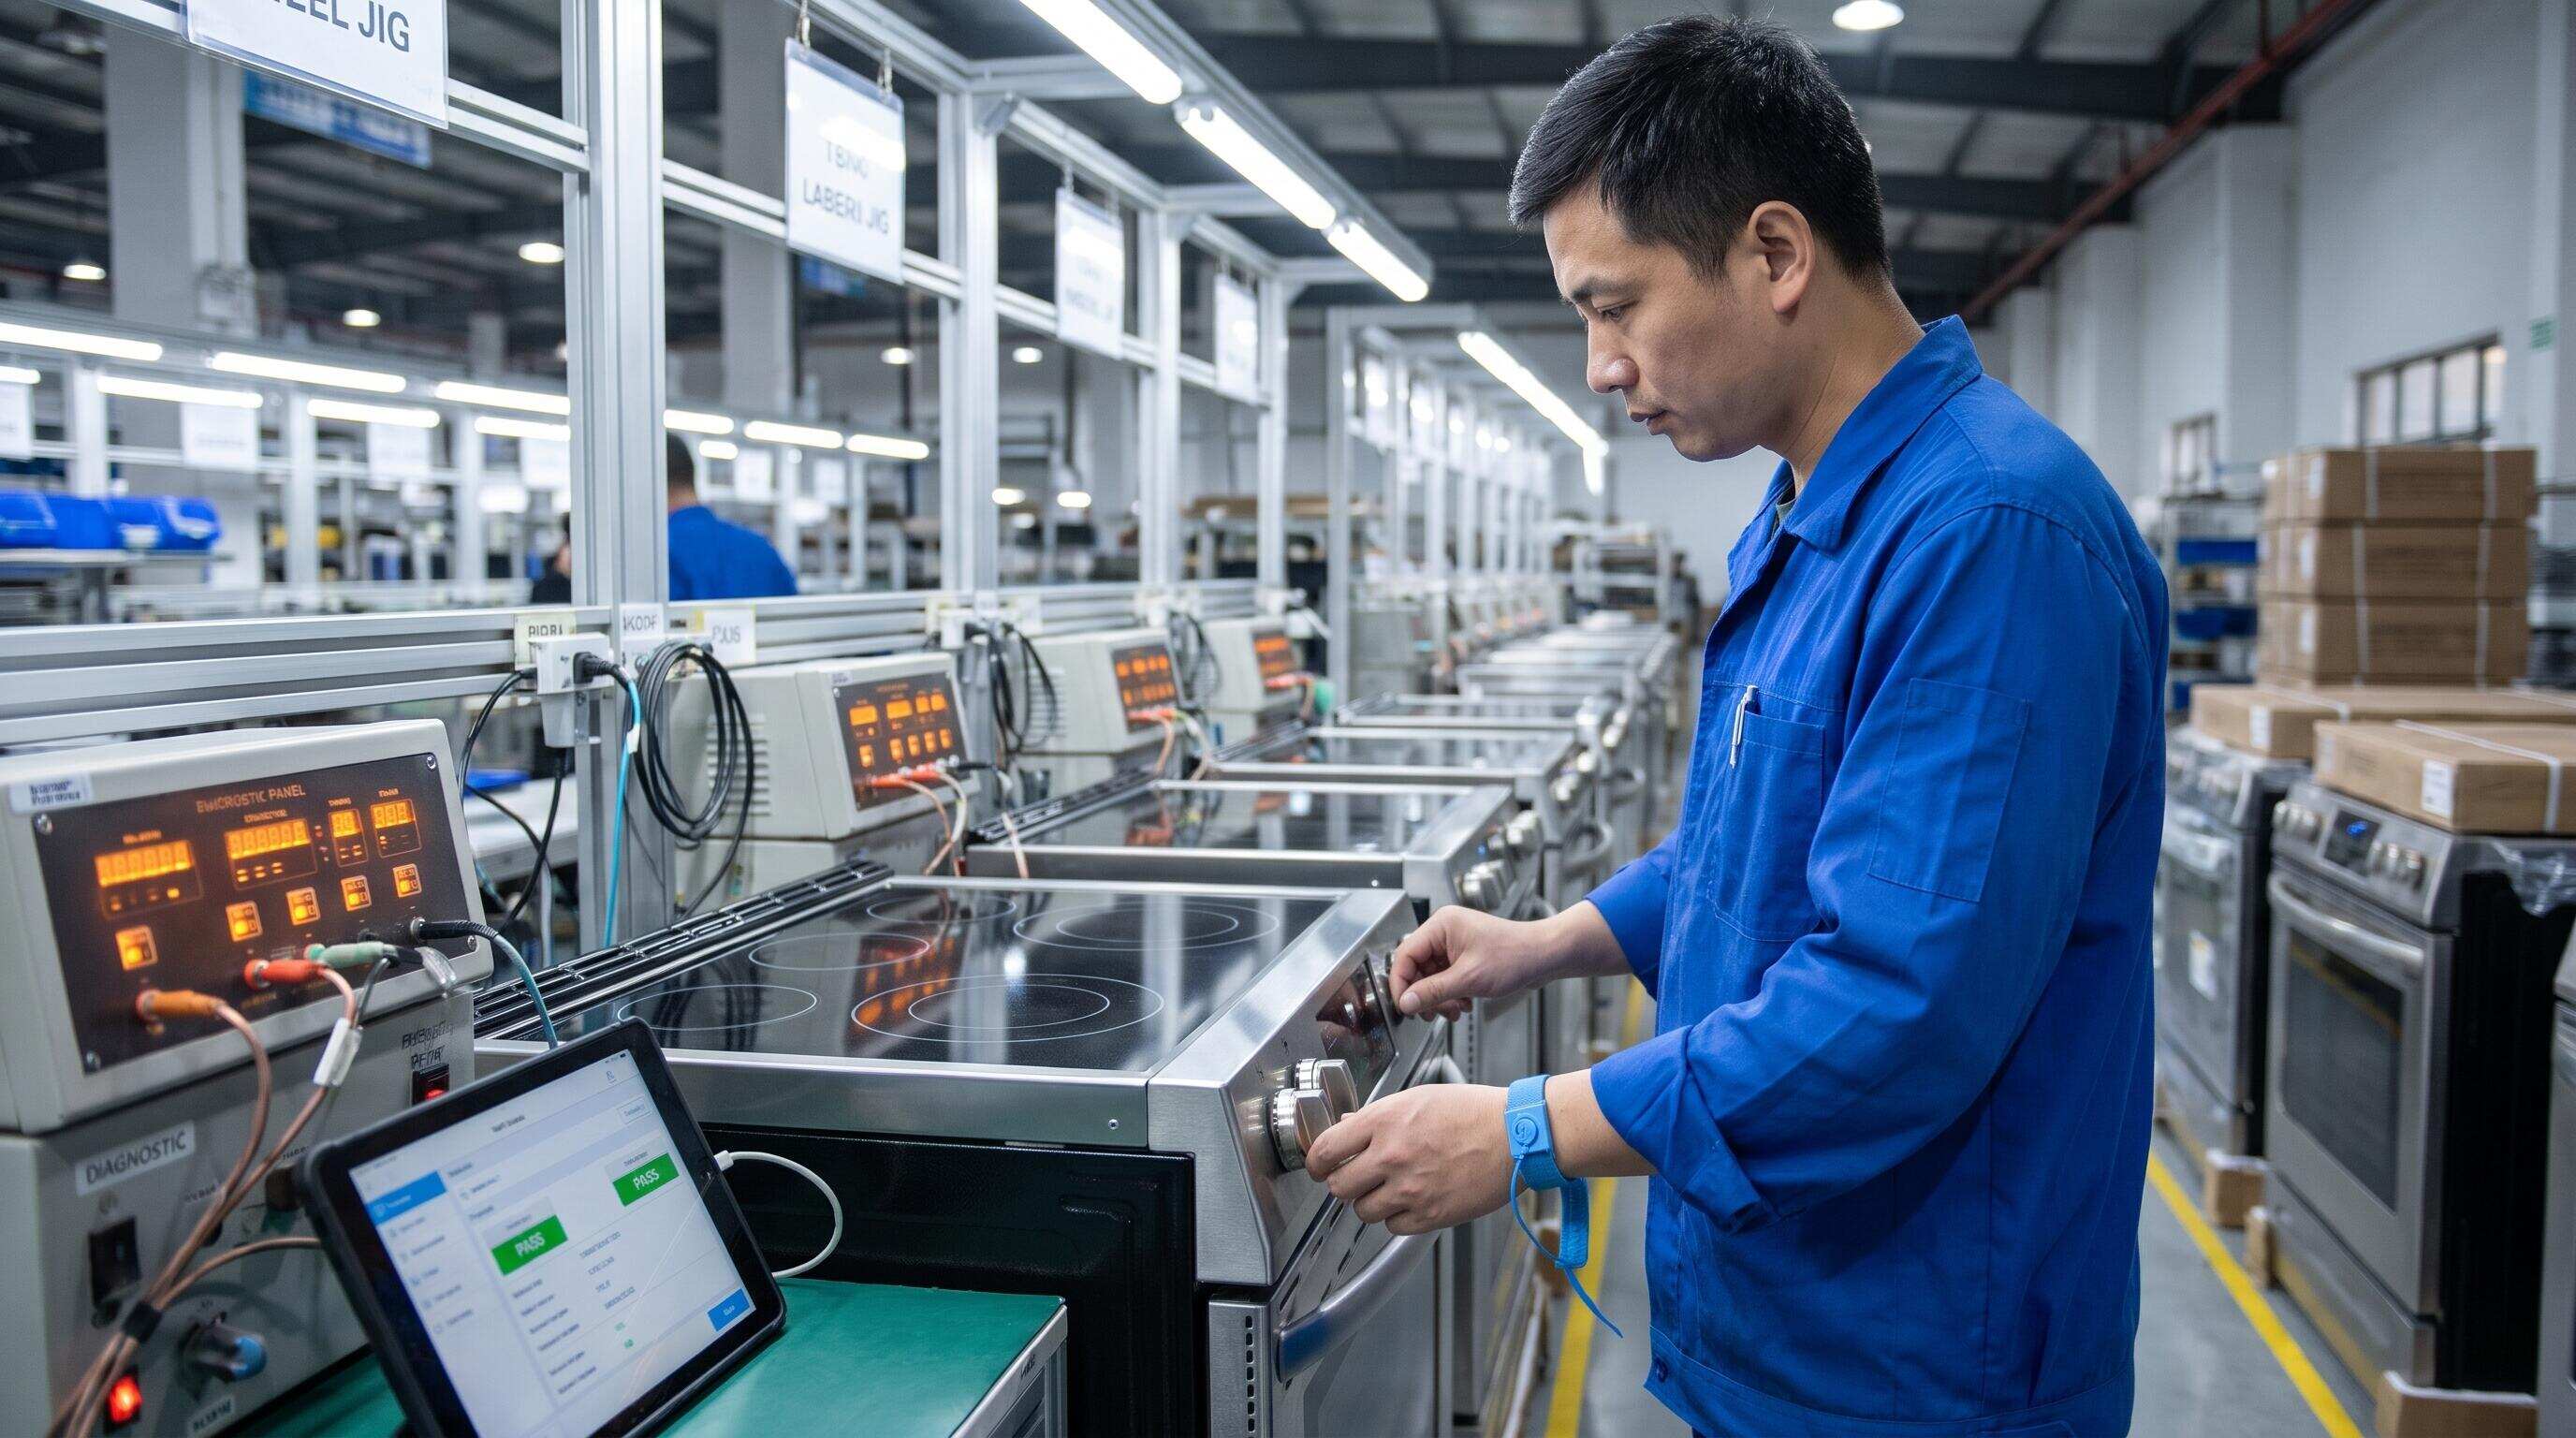
ALT: Inspector performing functional testing on smart kitchen appliance units at an OEM quality control station in a high-volume manufacturing facility
Advanced Considerations: Edge Cases, Misconceptions, and the Bigger Picture
Handling high-mix production without sacrificing quality consistency. One of the most demanding scenarios in OEM/ODM kitchen appliance manufacturing is the simultaneous production of multiple custom SKUs for different B2B clients. Each client's specifications differ — different combustion configurations, different control interfaces, different surface finishes. In this environment, a quality system designed only for high-volume single-SKU production will break down. Factories managing multiple customized SKUs should establish product-specific quality plans, inspection criteria, and test parameters. Where digital production systems are used, configuration controls can help ensure that the correct inspection requirements are applied when production switches between different models or product configurations.
Common misconception: a low defect rate at final inspection means quality is under control. A final inspection pass rate is a lagging indicator — it tells you what already happened, not what is happening. A factory that achieves a good final pass rate by investing heavily in end-of-line sorting and rework may actually have deeply unstable upstream processes. The cost of that instability is absorbed internally and may not be visible to a buyer reviewing audit reports. The right question to ask a factory is not only "What is your final inspection pass rate?" but "What is your first-pass yield before rework?" — a much more revealing metric.
Relationship with international certification and regulatory compliance. Different markets have different product safety and conformity requirements. For the EU market, manufacturers should identify the applicable directives and regulations and prepare the relevant EU Declaration of Conformity where required. For the U.S. and Canadian markets, buyers should verify the applicable safety standards and confirm that the relevant certification or listing covers the exact product model and configuration. Where the IECEE CB Scheme applies, buyers can review the relevant CB test documentation as part of their compliance assessment. The manufacturer's quality management processes should support consistent production of products within the verified compliance scope.
People Also Ask
Q1: How does a factory measure its inspection pass rate in appliance manufacturing?
In appliance manufacturing, factories typically track three distinct metrics that should not be conflated: (1) Lot Acceptance Rate, the percentage of production batches that pass sampling inspection (such as AQL criteria) at Final Quality Control (FQC); (2) FQC Unit Pass Rate, the percentage of finished units passing final inspection (which may include units that underwent earlier rework); and (3) First-Pass Yield (FPY), the percentage of units passing an in-process or final checkpoint on the first attempt without any rework or repair. Buyers should request both FQC pass rates and pre-rework FPY data—along with the sampling standard and calculation basis—to evaluate true process stability.
Q2: Are third-party inspections sufficient to verify a supplier's quality performance?
Third-party inspections — conducted by firms such as SGS, Bureau Veritas, or Intertek — are a valuable tool for independent verification, but they are not a substitute for a supplier's own embedded quality system. Third-party inspections are typically point-in-time events, often conducted on a sample of finished goods, and they can miss systemic process issues that only become visible through continuous monitoring. The most effective sourcing strategies use third-party inspection to validate and audit a supplier's internal quality system, not to replace it. Buyers should discuss audit scope, access arrangements, and documentation requirements with prospective suppliers. A supplier's willingness and ability to support an agreed audit can be one factor in the qualification process.
Q3: How long does it typically take to audit a Chinese appliance factory's quality system before placing a large order?
The time required to audit a Chinese appliance factory depends on the factory's size, the number of production lines, product complexity, audit scope, and the availability of quality records. Buyers should agree on the audit agenda in advance, allowing sufficient time for document review, production floor observation, equipment calibration checks, and corrective action record evaluation. For complex manufacturing operations, additional time may be necessary.
Wrapping Up
Achieving a benchmark inspection pass rate in high-volume appliance manufacturing is possible, but it requires a disciplined, layered quality architecture that prevents defects rather than simply detecting them after the fact. The key takeaways from this analysis are as follows:
- Prevention outperforms detection: the highest-performing factories control quality at the incoming material, in-process, and finished goods stages simultaneously, rather than relying on end-of-line sorting.
- Data is the differentiator: statistical process control and full production traceability transform quality from a reactive function into a predictive one, enabling consistent results across long production runs and multiple SKUs.
- Root cause closure is what makes high pass rates durable: factories that rigorously investigate and permanently resolve defect causes sustain their performance; those that only rework visible defects do not.
- First-pass yield is the honest metric: buyers should ask for pre-rework yield data, not just final inspection pass rates, to understand the true capability of a supplier's production process.
- Certification and quality capability are complementary: Product certifications, conformity documentation, and applicable regulatory requirements address different aspects of market access. Buyers should verify the relevant documents for each product model and destination market while separately evaluating the manufacturer's ability to maintain consistent production quality.
For procurement managers and sourcing specialists evaluating OEM/ODM partners in the smart kitchen appliance sector, the practical next step is to translate these principles into concrete supplier qualification criteria — and to audit prospective partners against them before committing to volume.
Looking for an OEM/ODM kitchen appliance manufacturing partner? Explore Hyxion's product capabilities and discuss your quality requirements, inspection criteria, and production specifications with the team. Request a customized quotation to learn more about the manufacturing and quality control arrangements available for your project. Visit the Hyxion website to explore smart kitchen appliance product lines, request a custom OEM/ODM quote, or connect directly with the Hyxion team to discuss your sourcing requirements and quality standards.
References
- International Organization for Standardization. "ISO 9001 — Quality Management Systems".
https://www.iso.org - International Electrotechnical Commission. "IEC Standards for Electrical Appliance Safety".
https://www.iec.ch - Underwriters Laboratories. "UL Product Safety Certification and Testing".
https://www.ul.com - National Institute of Standards and Technology. "Manufacturing Quality and Measurement Standards".
https://www.nist.gov
Note: Standards may be updated; please check the latest official documents or consult professional advisors.